Start with the materials, not the adhesive
The first question in adhesive selection is what, exactly, needs to be joined. “Plastic” is not one material: rigid acrylic, flexible vinyl and low-surface-energy plastics can behave very differently. Wood varies with grain direction, moisture and finish. Metals may arrive with oil, oxide or a coating between the adhesive and the underlying material. Identify both substrates as specifically as possible, including any paint, plating or laminate that will remain in the finished joint.
An adhesive must wet the surfaces to make useful contact. Dust, release agents, grease and loose coatings can prevent that contact even when the adhesive is otherwise suitable. Many plastics and elastomers need a product formulated for them, and some may require a primer or surface treatment. Check the adhesive maker’s substrate guidance before choosing a product; broad claims such as “bonds everything” are a poor substitute for compatibility with the actual surfaces.
Read the load and the shape of the joint
A joint’s strength depends on how force passes through it. Adhesive bonds generally make better use of a broad overlap than a narrow edge-to-edge contact. A lap joint spreads force across an area, while a butt joint can concentrate it at a small section. Where possible, design parts to locate one another mechanically so the adhesive does not have to resist every force on its own.
Pay particular attention to peel and cleavage: forces that lift one edge or pry a joint apart. A bond that performs well under evenly distributed shear may fail much sooner when pulled from an edge. Also distinguish a steady load from repeated vibration, impacts or bending. A rigid adhesive may suit parts that must stay precisely positioned, while a more flexible bond may better accommodate movement between materials. Neither property is automatically better; it must match the joint.
Account for the working environment
Think beyond the moment of assembly. Will the product encounter water, cleaning chemicals, sunlight, heat or cold? Will its parts expand and contract at different rates? A bond that seems firm on the bench may be unsuitable after repeated temperature changes or prolonged exposure to moisture. Use the adhesive’s stated service conditions as a screening tool, and pay attention to whether those conditions describe brief exposure or continuous use.
Assembly conditions matter too. Some products require a close-fitting joint; others can tolerate a specified gap. Cure time may differ from handling time, and temperature or humidity can affect the process. Consider whether the workshop can hold parts in place for the required period and apply a consistent amount of adhesive. Choosing a product that fits the available process is often more useful than choosing one with the most impressive-sounding strength claim.
Narrow the options by adhesive family
Adhesive families offer a starting point, not a universal ranking. Wood glues are often convenient for close-fitting wood joints. Epoxies can be useful where a bond must accommodate a modest gap, though their properties vary widely. Cyanoacrylates can set quickly on small, well-fitting parts but may not suit joints exposed to repeated impact or movement. Flexible sealant-adhesives can help where movement is expected, provided the design can accommodate their bond thickness and cure requirements.
Pressure-sensitive tapes and films deserve consideration when a clean, uniform bond line or fast assembly matters. Their performance depends heavily on surface preparation, application pressure and the intended load. For any family, compare products using the same questions: Are both substrates listed as compatible? Is the product suited to the joint geometry and service environment? Can the workshop follow its preparation, application and cure instructions reliably?
Prepare, test and document the bond
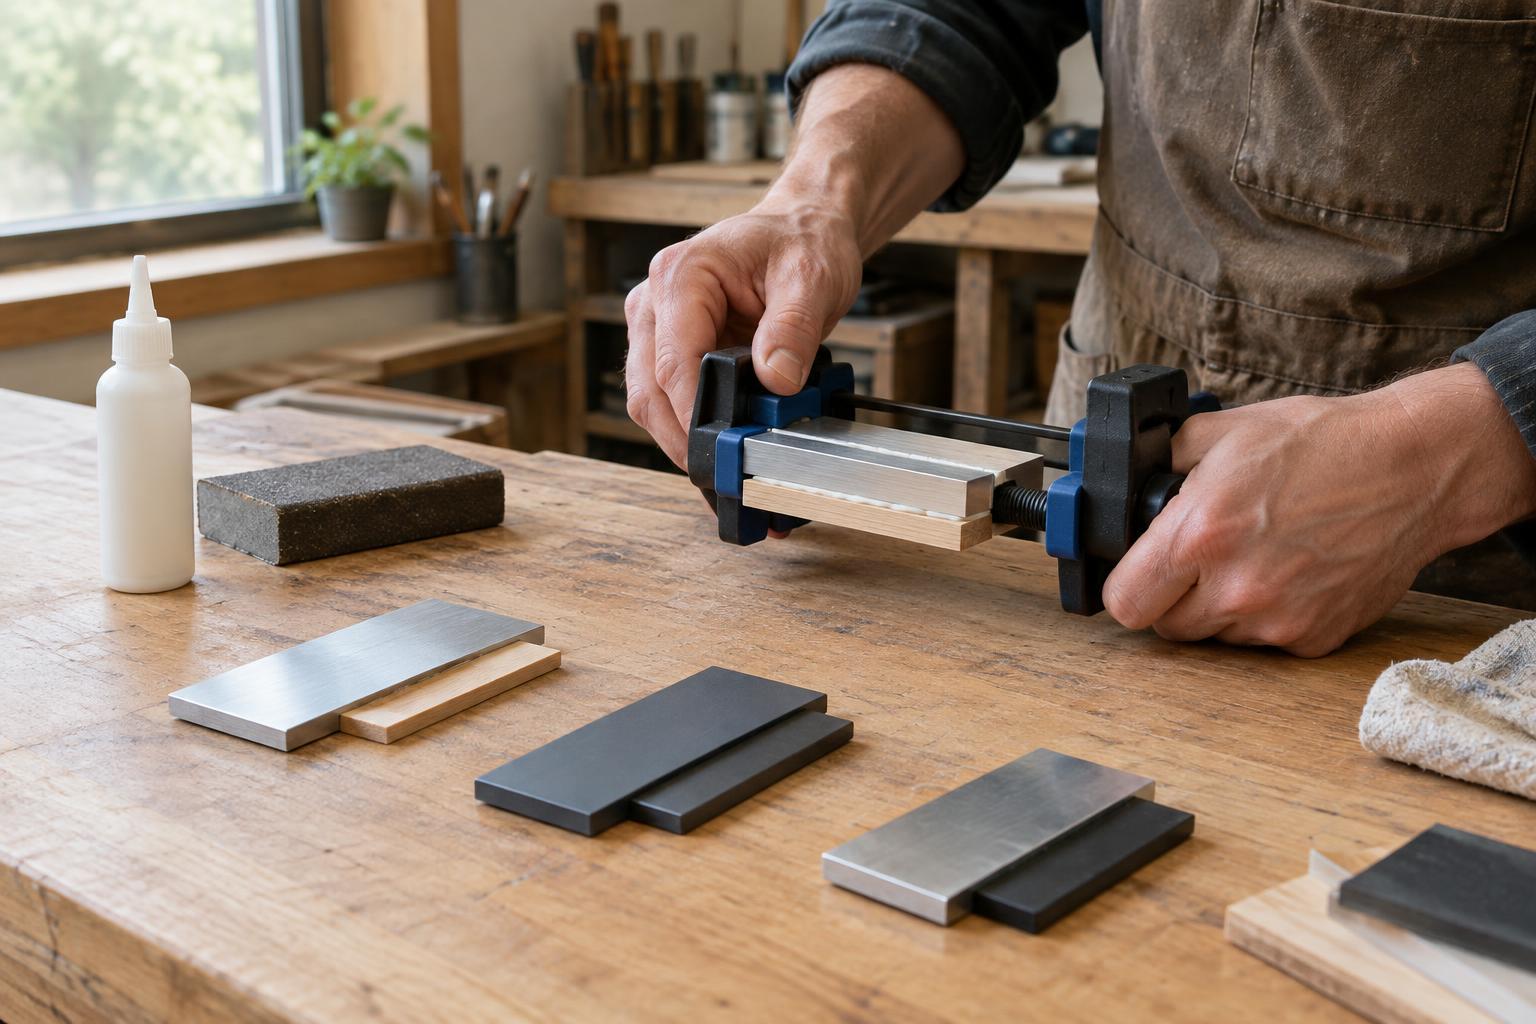
Once a candidate is chosen, prepare sample joints using the real materials and the proposed production method. Clean surfaces as directed, and remove loose finishes or contamination rather than bonding over them. If sanding, priming or another treatment is specified, apply it consistently. Follow the product instructions for mixing, bond-line thickness, clamping, ventilation and cure; changing several variables at once makes a failed test difficult to interpret.
Test samples in ways that resemble their intended use. Pulling a sample apart by hand may reveal an obvious weakness, but it does not establish a reliable load rating. Look at where failure occurs: within the adhesive, at its interface with a surface, or within the substrate itself. Record the materials, preparation steps, adhesive, cure conditions and observations. That small process record helps a workshop repeat a successful bond—and recognize when a material or design change calls for a new test.